

Understanding the Benefits of Quality Fiber Reinforced Diaphragms in the Chemical Industry
Publish:
2026-04-23


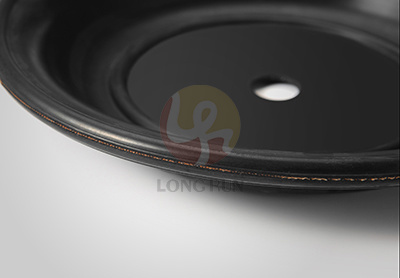
Fiber reinforced diaphragms have become increasingly essential in the chemical industry due to their unique properties and performance benefits. These diaphragms are engineered with a combination of fibers and polymer materials, resulting in enhanced strength, durability, and flexibility compared to traditional diaphragm materials. This article delves into the practical knowledge surrounding quali
Fiber reinforced diaphragms have become increasingly essential in the chemical industry due to their unique properties and performance benefits. These diaphragms are engineered with a combination of fibers and polymer materials, resulting in enhanced strength, durability, and flexibility compared to traditional diaphragm materials. This article delves into the practical knowledge surrounding quality fiber reinforced diaphragms, discussing their composition, applications, and key advantages for professionals in the rubber and chemical sectors.
One of the primary characteristics of quality fiber reinforced diaphragms is their superior mechanical strength. The incorporation of fibers—such as glass, aramid, or carbon—provides reinforcement, enhancing the diaphragm's ability to withstand high pressures and cyclic loading conditions. This feature is particularly beneficial in applications involving pumps and valves, where reliability and longevity are paramount.
In addition to mechanical strength, quality fiber reinforced diaphragms demonstrate excellent chemical resistance. This makes them suitable for use in aggressive environments where exposure to harsh chemicals and solvents is common. The right combination of polymer matrix and reinforcing fibers allows these diaphragms to maintain their integrity and performance over time, even in challenging conditions.
Another advantage of using quality fiber reinforced diaphragms is their versatility. They can be designed to meet specific requirements, such as varying thicknesses, shapes, and sizes, providing tailored solutions for different applications. This adaptability makes them suitable for a wide range of uses within the chemical industry, from sealing systems to pressure regulation.
When selecting a fiber reinforced diaphragm, it's crucial to consider several factors to ensure optimal performance. First, assess the specific chemical compatibility required for your application. Not all fiber and polymer combinations are suitable for every chemical exposure, so understanding the chemical environment is critical. Second, evaluate the operational conditions, including temperature and pressure ranges, to select a diaphragm that can withstand the expected stresses.
Furthermore, quality control during the manufacturing process plays a vital role in the performance of fiber reinforced diaphragms. Ensuring that the materials used are of high quality and that the production processes meet industry standards will contribute significantly to the reliability and durability of the diaphragms.
In conclusion, quality fiber reinforced diaphragms offer numerous advantages for professionals in the chemical industry, including enhanced strength, chemical resistance, and versatility. By understanding their properties and the factors influencing their performance, industry personnel can make informed decisions that contribute to the efficiency and reliability of their applications. Emphasizing quality in the selection and manufacturing of these diaphragms is essential for achieving optimal results in various industrial settings.
Related News
The Role of Rubber Bonded Metal Products in Improving Industrial Efficiency
The Role of Rubber Bonded Metal Products in Improving Industrial Efficiency Table of Contents Introduction Understanding Rubber Bonded Metal Products Historical Development of Rubber Bonded Metal Technology Benefits of Rubber Bonded Metal Products Applications in Industrial Settings Impact on Industrial Efficiency Future Trends and Innovations Frequently Asked Ques
Oct 12,2026
The Essential Guide to Viton O-Rings: Key Benefits and Applications
Viton O-rings are vital components in various industrial applications, particularly in the chemical and rubber products sector. Known for their exceptional performance, these O-rings are made from a type of fluoroelastomer that exhibits remarkable resistance to heat, chemicals, and aging. This unique combination of properties makes Viton O-rings an ideal choice for demanding environments where tra
Oct 09,2026
The Benefits of Choosing Molded Rubber Balls Over Traditional Alternatives
The Benefits of Choosing Molded Rubber Balls Over Traditional Alternatives Table of Contents Introduction Understanding Molded Rubber Balls Advantages of Molded Rubber Balls Durability and Longevity Cost Efficiency Customizability Versatility in Applications Environmental Impact Comparison with Traditional Alternatives Selection Criteria for Molded Ru
Oct 06,2026
Unlocking the Versatility of Rubber Balls in the Chemical Industry
Rubber balls are a remarkable example of how a simple concept can manifest in numerous applications within the chemical sector and beyond. Their versatility makes them an essential component in various industries, including manufacturing, automotive, and sports. Understanding the properties and potential uses of rubber balls can empower businesses to harness their capabilities effectively. First a
Oct 03,2026
The Vital Role of Rubber Flexible Connectors in Modern Industrial Systems
The Vital Role of Rubber Flexible Connectors in Modern Industrial Systems Rubber flexible connectors are essential components in various industrial applications, playing a crucial role in facilitating the seamless operation of systems that rely on fluid and gas movement. In today's fast-paced industrial landscape, the significance of these connectors cannot be overstated. As industries evolve and
Sep 30,2026
Add: Building # 7, No. 27, Songbai Ling Avenue, Zhonghan Huizhou Industrial Park, Zhongkai High-tech Zone, Huizhou, Guangdong, China 516032

LONGRUN
Privacy Policy | SEO | Support: 300.cn